
A scientific breakthrough may create a pathway toward a promising therapy, but bringing that treatment to patients can involve months of coordinated manufacturing, testing, and quality reviews. For advanced therapies, production capacity, specialized equipment, raw material availability, and manufacturing costs can all affect how quickly a treatment reaches patients.
According to Alira Health’s 2026 Biologics Contract Manufacturing Report, the global biologics contract manufacturing market reached $23.2 billion in 2025, with investment increasingly focused on specialized manufacturing capabilities. These findings highlight why manufacturing expertise and infrastructure deserve early attention as therapeutic development progresses.
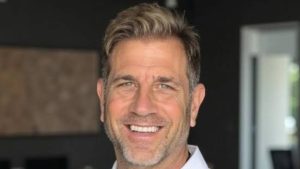
For Mike Stewart, founder and CEO of Soter Bio, a U.S.-based contract development and manufacturing organization (CDMO) specializing in advanced biologics, including mRNA, cell therapy, gene therapy, and plasmid DNA, manufacturing readiness is a fundamental part of therapeutic innovation. With 24 years of experience in biopharmaceutical development and operations, Stewart emphasizes the connection between scientific advancement and practical delivery. “The most important lesson is to solve the whole problem,” he explains. His perspective highlights the importance of bringing together process development, quality assurance, supply-chain planning, and patient access.
This approach is particularly important in mRNA manufacturing, where product quality relies on several interconnected processes. Manufacturers must often maintain control over RNA identity, integrity, purity, and biological activity while overseeing formulation, filling, storage, and transportation. Stewart points out that lipid nanoparticle formulations bring additional quality considerations, including particle characteristics and encapsulation.
A 2026 review in Molecular Biology Reports, indexed by Springer Nature, explores the process controls and analytical methods that help maintain product quality. These requirements demonstrate why manufacturing readiness relies on coordinated expertise throughout production and testing.
Personalized cancer vaccines introduce another layer of complexity, as each patient may need an individually tailored product and a corresponding production schedule. Traditional timelines can involve documentation, material procurement, manufacturing, testing, and release. When these activities are managed by separate teams or external providers, scheduling requirements and handoffs can further extend the process. Stewart explains, “The full manufacturing pathway deserves attention, since improvements within a single production step may have limited effects on the total time from patient-specific design to treatment.”
Soter Bio’s personalized vaccine manufacturing model is designed to significantly shorten end-to-end timelines compared with conventional approaches. This distinction is important because sequence-to-product processing time is not the same as the complete period between a patient’s biopsy and treatment administration. Stewart stresses that clearly defined measurements and documented results allow developers to better evaluate the practical impact of manufacturing efficiency improvements.
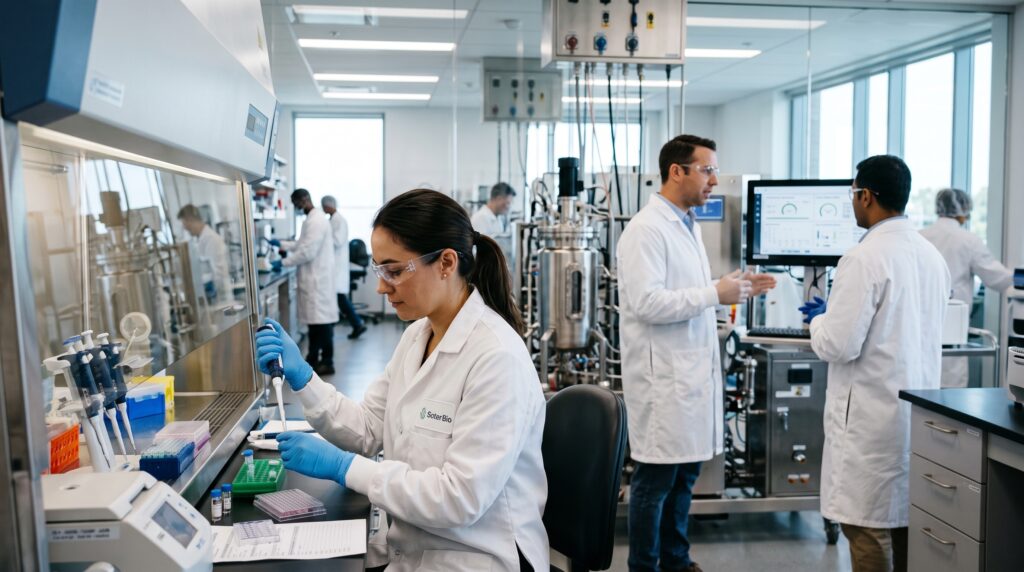
Improving efficiency may rely just as much on process coordination as on production technology. Closed manufacturing systems can minimize contamination risks during handling, while automation may improve consistency and reduce manual interventions. In-line analytics can also deliver timely insights into process conditions, allowing teams to identify potential deviations earlier.
Stewart’s operational experience also underscores the importance of preparing for production well before a manufacturing campaign begins. Documentation, quality agreements, raw material procurement, and sample planning can account for considerable portions of the overall timeline. Having appropriate materials available and reusable documentation frameworks in place may help eliminate unnecessary preparation delays.
“A target, a modeled estimate, and a demonstrated result are different things,” Stewart remarks. “Efficiency targets become more informative when supported by repeatable performance data and clearly defined endpoints.”
The potential applications extend beyond personalized cancer treatments. Flexible manufacturing platforms could also support animal-health vaccines and therapeutics, where production costs and batch requirements may affect development and supply. They could also play a role in pandemic preparedness by strengthening the development, testing, and production capabilities needed as public-health demands evolve.
The World Health Organization’s mRNA technology transfer program offers a relevant example of international efforts to expand manufacturing knowledge and regional production capabilities. Achieving these potential benefits requires product-specific validation, appropriate regulatory oversight, and infrastructure capable of accommodating different manufacturing needs.
Investment continues to play a significant role in this process. “When people look at advanced therapy manufacturing, they often focus strictly on floor space, but that’s only part of the equation,” Stewart says. “True operational capacity depends on specialized testing, ready-to-go processes, proper materials, and expert talent. Setting all of that up takes substantial capital upfront, often months or years before a program starts generating revenue.”
At Soter Bio, which is developing U.S.-based manufacturing infrastructure for advanced biomolecules and active pharmaceutical ingredients, these factors help shape the case for more coordinated domestic production capabilities. Closed, automated systems and scalable infrastructure may strengthen supply resilience, while early investment in testing and quality operations can help ensure production capacity meets batch-release requirements. Stewart believes investment decisions should begin by identifying the constraints most relevant to a particular program, whether they involve equipment, testing capacity, documentation, or material availability.
Manufacturing improvements may also contribute to affordability by reducing duplicated work, making better use of resources, and minimizing unnecessary delays. However, their influence on patient access also depends on clinical evidence, regulatory requirements, reimbursement, treatment delivery, and healthcare financing. Reduced production costs may create opportunities to expand access, although the actual benefits will depend on decisions made throughout therapeutic development and the wider healthcare system.
For biotech leaders and investors, manufacturing readiness may therefore deserve attention from the earliest stages of therapeutic development. Developers, CDMOs, analytical teams, and regulatory specialists can work together on process transfer, material availability, testing strategies, and future production needs before these considerations become urgent. Investors can help advance this work by supporting process development, validated analytical methods, infrastructure, and skilled personnel alongside scientific research.
“Discovering new science gives patients hope, but reliable manufacturing is what makes that hope actionable,” Stewart remarks. “By viewing manufacturing readiness as a critical development milestone rather than an afterthought, and investing in repeatable quality, biotech leaders can improve their chances of getting life-changing therapies to patients within meaningful timeframes.”